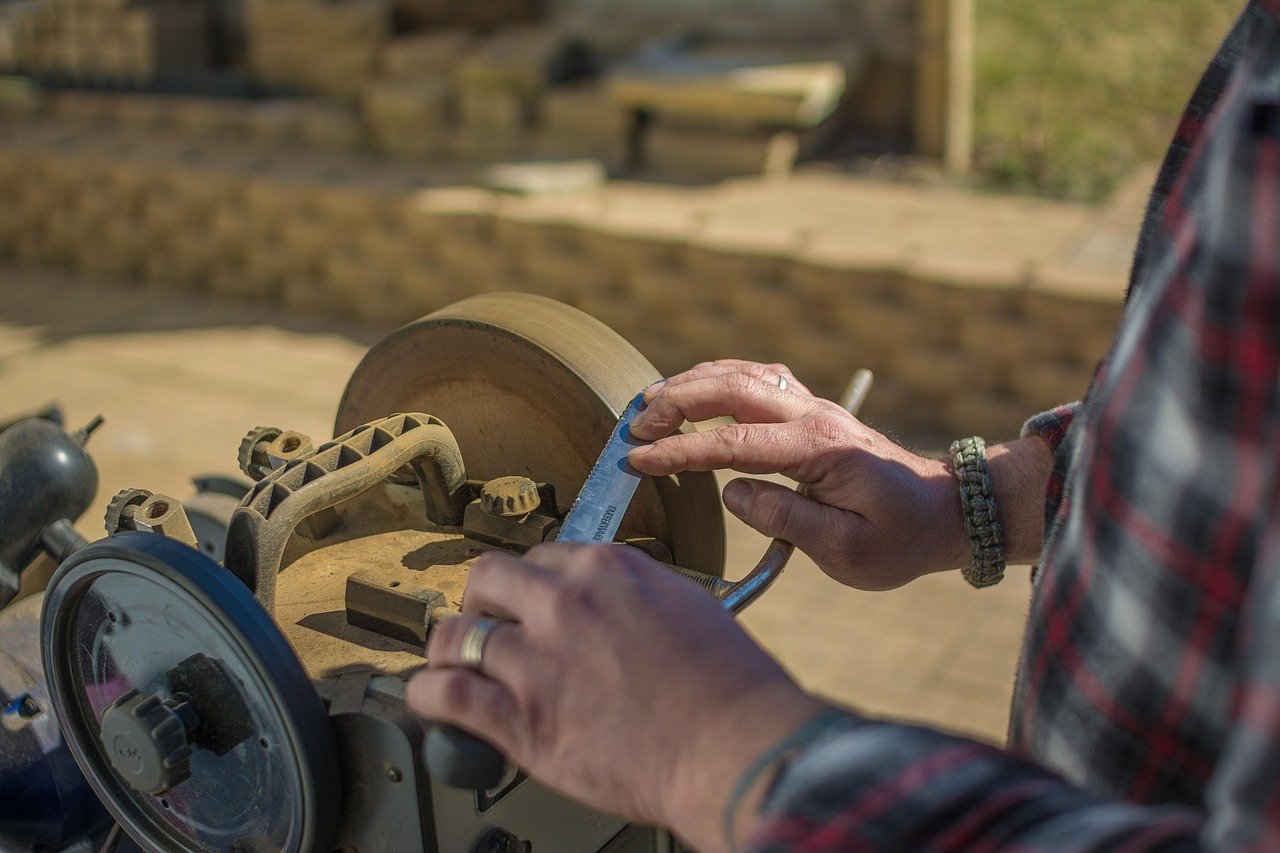
An efficient sharpening sequence may use fewer stones than the rack suggests.
A kitchen knife that still cuts paper but slips on tomato skin needs less abrasion than one with chips, a rolled apex, or a bevel that needs resetting. Putting both on a coarse stone removes unnecessary steel; taking a damaged edge straight to a finishing stone merely polishes unresolved geometry.
Inspect the apex under bright light, then test it gently on its intended material. Use coarse grit for damage or geometry changes, advancing only after a consistent apex forms. For touch-ups, start medium or fine. Stop at a task-appropriate finish: toothier for fibrous foods, more polished for push-cutting.
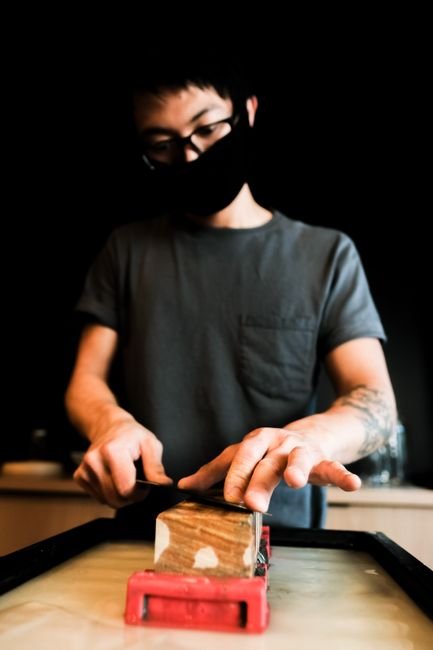
Inspect the edge before choosing a grit
Hold the clean, dry edge under a bright light and slowly rotate it. A properly apexed section reflects little light; bright points or lines can indicate flattened areas, chips, or a rolled edge. View both sides, since a roll may lean away and disappear from one angle.
Use magnification only when reflected light and a cutting check leave the problem unclear. A loupe can help distinguish a chip from stubborn burr material, but it should not replace inspection along the full edge.
Classify the work by required steel removal:
- Repair or reprofiling: visible chips, pronounced rolls, an overly thick edge, or uneven bevels that need correction. Start relatively coarse.
- Routine sharpening: no major damage, but the edge reflects light or slips on paper, tomato skin, or similar material. Begin at a medium grit.
- Touch-up: geometry remains sound and only crisp bite has faded. Use a fine stone or strop.
Coloring the bevel with permanent marker reveals whether each stroke reaches the apex.
Start only as coarse as needed
Choose the finest abrasive that can still restore the apex in a reasonable number of passes. Within DMT’s own grit scale, Coarse (325 mesh) is a plausible starting point for substantial bevel correction, while Fine (600 mesh) may suit routine sharpening; these are starting examples, not equivalents for other brands (DMT, Grit Guide).
Steel and abrasive type change the result. Diamond or CBN generally cuts high-vanadium, wear-resistant steels more readily, while aluminum oxide often works efficiently on simpler steels. Stone hardness, loading, pressure, and grit standards also affect cutting speed, so numbers from different systems should not be treated as interchangeable.
Stay at the starting grit until the bevel reaches the apex along the entire edge and the scratch pattern is consistent. Move finer once that work is complete. If controlled passes produce little visible change—or a chip or thick shoulder remains—reset one step coarser rather than consuming a finer abrasive.
Mark the bevel with permanent marker. Abrasion above the edge means the apex has not been reached; adjust the angle before changing grit.
Keep grit systems separate
A “1000 grit” stone is not automatically equivalent to every other 1000-grit abrasive. JIS R 6001, FEPA, and ANSI/CAMI use different grading rules and particle-size distributions. Micron ratings describe particle size more directly, but a single nominal figure may not reveal the full distribution. Proprietary labels can add another layer of ambiguity.
Bond hardness, abrasive type, and particle shape also affect cutting speed and scratch depth. Consequently, conversion charts should be treated as approximations—not permission to substitute labels blindly. When mixing products, consult the manufacturer’s particle-size data or the relevant JIS, FEPA, or ANSI standard.
A simpler approach is to stay within one documented product line. For example, using Naniwa Professional labels only, compact frameworks might be:
- Repair: 400 → 800 → 3000
- Routine sharpening: 800 → 3000
- Touch-up: 3000 alone
These are starting frameworks rather than fixed recipes. Add an intermediate stone if scratches remain deep; skip a step when the next stone removes them promptly. Major chips may require a coarser abrasive, while a toothy working edge may finish at 800 instead of continuing finer.
Prepare the abrasive without wasting it
-
Stabilize the station
Place the stone on a nonslip base with clearance for fingers and the knife tip.
-
Use specified lubricant
Follow the maker’s instructions; stones may require water, oil, or dry use.
-
Clear loading promptly
Remove swarf by the approved method. Loading slows cutting and encourages wasteful pressure.
-
Check flatness
Use a straightedge or pencil grid; dress dishing with the tool specified for that abrasive.
-
Clean between grits
Wipe the blade, hands, holder, and bench. Stray coarse particles can mimic unfinished scratches.
Keep fingertips above the spine or on the blade face, never ahead of the edge. Use controlled strokes and moderate pressure. Re-secure a wet base immediately if it starts sliding.
Form the apex before changing grits
Treat the starting grit as complete only when the bevel reaches the apex from heel to tip. Color the bevel with a permanent marker, then inspect under magnification: ink remaining near the edge indicates that more work is needed.
Maintain a stable sharpening angle on the stone so each pass deepens the same bevel instead of rounding it. Near completion, change the stroke direction slightly; fresh scratches should extend consistently to the edge along its full length.
Check for a burr carefully by moving a cotton swab or fingertip away from, never along, the edge. A continuous burr should form on the opposite side and switch sides when sharpening changes. Because burrs can break off or remain localized, confirm them with the marker and scratch pattern. Finish with lighter pressure to limit oversized burrs, deep scratches, and unnecessary steel removal.
Balance both bevels
Alternate sides before one bevel gets far ahead. Make three to five controlled strokes, switch faces, and preserve the same angle and stroke length. Near the apex, alternate after every stroke. Maintain this side-switching rhythm through each grit so later abrasives refine both bevels evenly.
Reduce pressure or time on the starting grit if the burr becomes large, one bevel grows visibly wider, or deep scratches persist on one face. These signs indicate excess metal removal, not faster sharpening.
Use a repeatable transition loop
At every new grit, clean the blade, stone, holder, and work area so loose coarse particles cannot score the bevel. Change scratch direction where practical; the contrasting pattern makes remaining scratches easier to spot.
Use normal sharpening pressure initially, then reduce it as the new pattern develops. Inspect the bevel heel to tip under bright, angled light. Advance only when the current grit has replaced the previous pattern across both bevels.
If one coarse scratch remains, work only that area with the current grit, blend it with several full-length passes, then inspect again. Restarting the entire progression usually wastes abrasive unless contamination or geometry errors affect most of the bevel.
Why is the stone cutting slowly?
Clean loading from the surface and confirm the abrasive is flat and appropriate for the steel. If scratches barely change, the grit jump may be too large.
What causes an uneven polish?
Uneven pressure, inconsistent angles, or incomplete scratch replacement commonly leave mixed finishes. Return one grit only where necessary and use lighter blending passes.
Why do deep scratches suddenly appear?
A loose coarse particle or damaged abrasive may be responsible. Stop, clean everything, inspect the surface, and resume at the grit that can remove the scratch efficiently.
Why does the abrasive load rapidly?
Swarf buildup often increases with heavy pressure or inadequate lubrication. Clean more frequently and use the lubricant specified by the abrasive manufacturer.
Why does the burr keep flipping sides?
Pressure may be too high or the burr too large. Alternate single passes with progressively lighter pressure until it weakens, then deburr.
Stop at the grit the job requires
A coarser finish retains microscopic teeth that can help with rope, cardboard, fibrous foods, and other slicing cuts. Greater refinement generally suits push cutting, fine food preparation, and tasks where a cleaner cut matters. Because grit standards differ, judge the result by scratch refinement and cutting behavior rather than a universal finishing number.
A mirror bevel is not automatic proof of sharpness. Polishing can make the bevel reflective while leaving the apex rounded, incompletely formed, or burdened by a foil burr.
Confirm the endpoint under strong light or magnification: the apex should show no bright, flat spots, and the intended test material should cut cleanly without snagging. Paper can provide a controlled check; fingers should never be drawn along the edge.
Once the entire edge is apexed, use short, alternating passes with steadily lighter pressure. Then concentrate on removing the final burr, switching sides frequently so it is abraded away rather than folded back and forth. Recheck both sides under light and repeat only the minimum number of passes needed.
- Assign the job Before using an abrasive, define its task: repair damage, reach the apex, replace scratches, remove the burr, or refine the finish.
- Verify the exit Change grits only after a visible check confirms completion, such as continuous apexing, a replaced scratch pattern, or burr removal.
- Skip redundancy If a stage has no distinct purpose or inspection standard, omit it. Extra steps consume abrasive without resolving a known problem.
- Build a record Record each successful progression so later maintenance can start finer and use fewer passes.
Make every grit earn its place
- Log the knife, steel, abrasive brand and system, starting grit, finishing grit, pressure changes, and cutting result.
- On the next touch-up, begin one stage finer when the edge has no chips or geometry problems; move coarser only if progress is inadequate.
A practical pocket knife sharpening process can be reduced to one decision rule: each abrasive must have a defined job and an observable exit condition. Before every stage, state what must change; afterward, inspect the edge under consistent light and confirm that change before continuing.
This turns grit progression into a repeatable protocol rather than a fixed ladder. Records reveal which steels, edge geometries, and finishes respond well to particular abrasives, reducing guesswork and unnecessary wear during future maintenance.
Progression matters most when there is real metal to remove, which is the situation set out in how to remove chips from a knife edge — that is where skipping a coarse stone costs the most time.